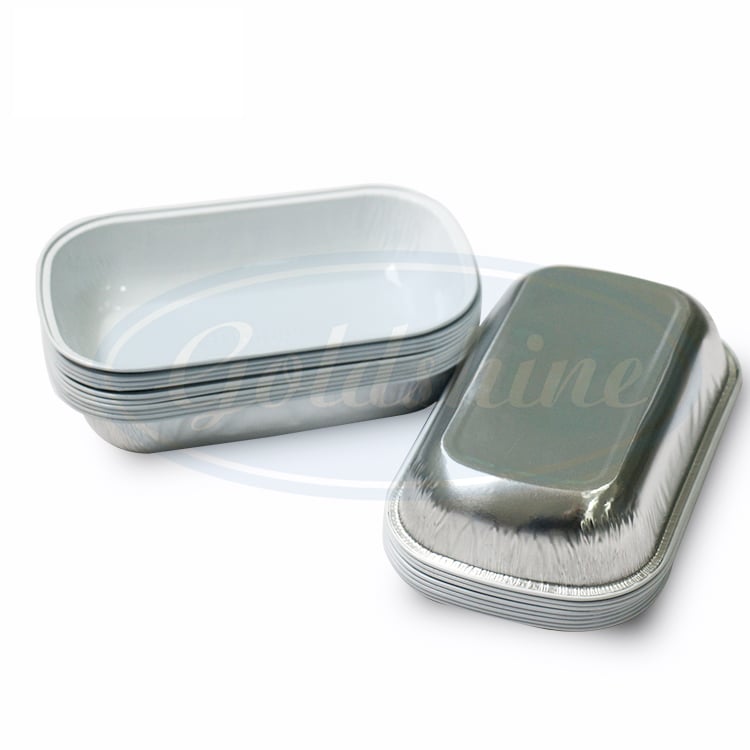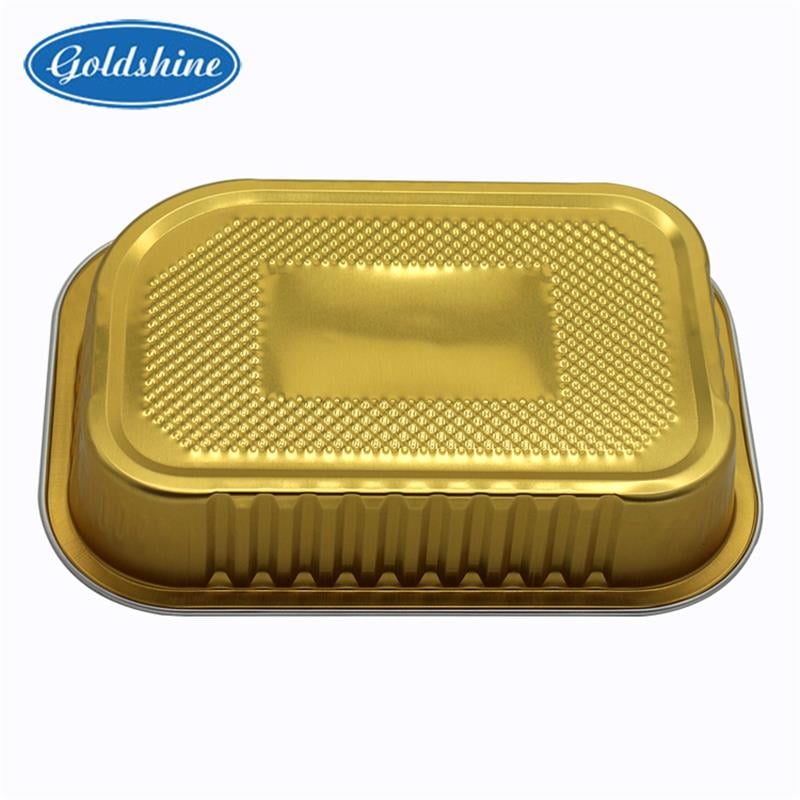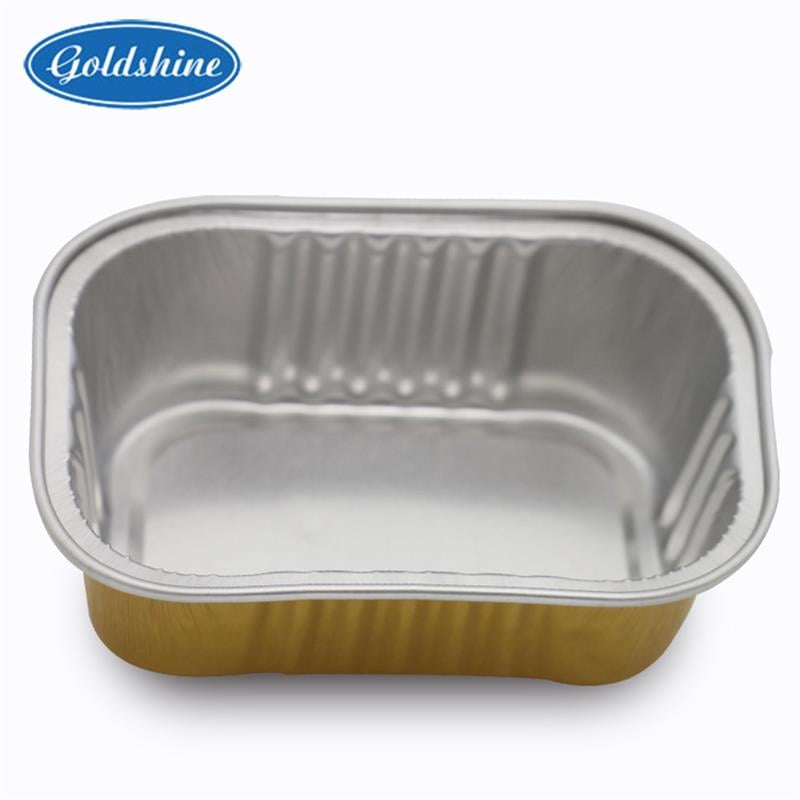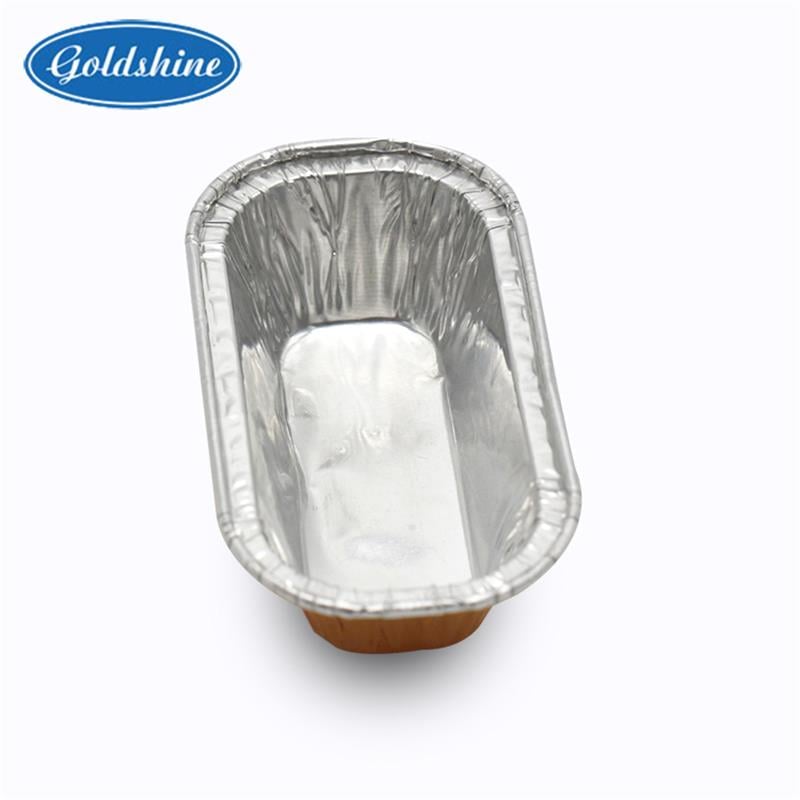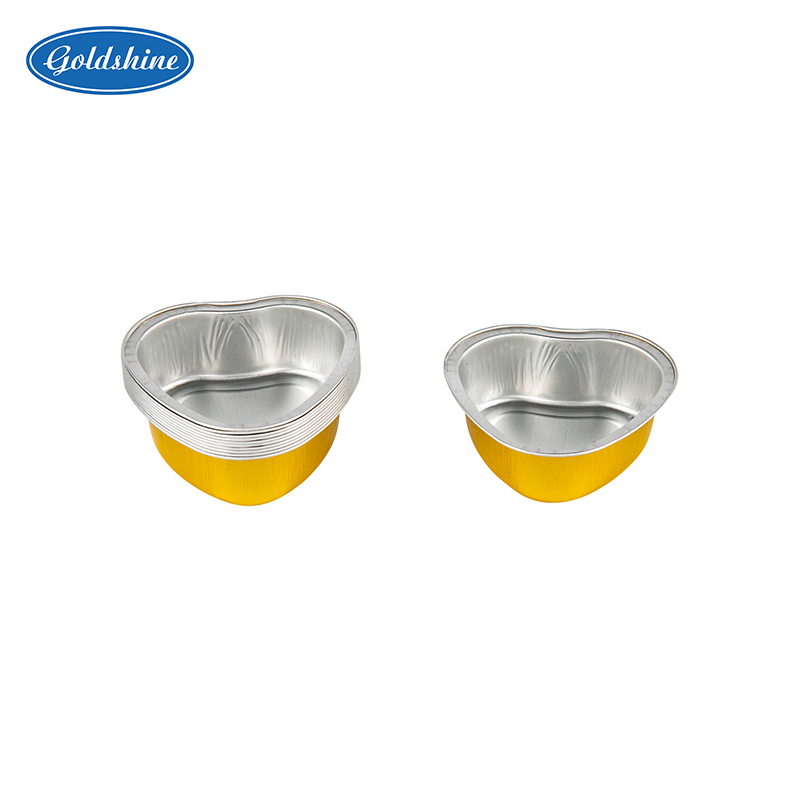
Aluminium foil containers are versatile packaging solutions widely used in the food industry for cooking, baking, and food preservation. As a B2B buyer, selecting the right aluminium foil container box is crucial to ensuring product safety, maintaining quality, and optimizing operational efficiency. This article will address key considerations for choosing jumbo roll aluminium foil container boxes, including specifications, quality evaluation, applications, and the advantages of sourcing from a trusted manufacturer like Goldshine.
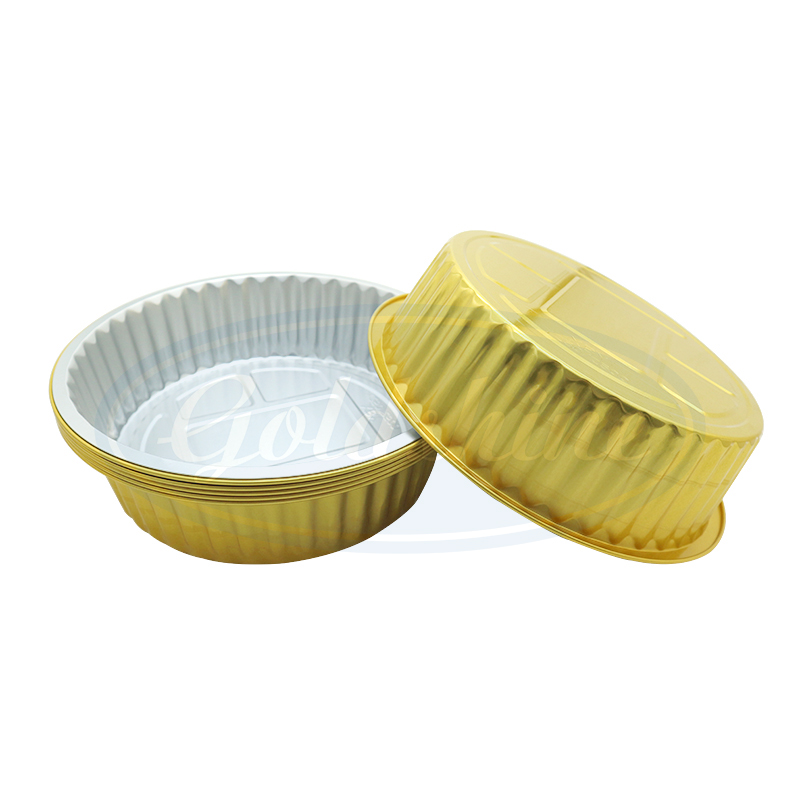
When selecting an aluminium foil container box, consider its intended use, material properties, and compatibility with your production processes. First, determine the specific application—whether it’s for baking, storage, or takeaway food packaging. The design, such as depth and size, should align with your product dimensions to avoid spillage or spoilage.
Aluminium foil containers come in various shapes and thicknesses. Thicker containers generally offer better structural integrity and heat resistance, making them suitable for oven use. Conversely, lightweight options may be preferable for cold storage and takeaway applications. Be sure to communicate your specific needs regarding these parameters to ensure the product fits your operational requirements.
Several specifications are critical when evaluating aluminium foil containers:
Material Thickness: Typically measured in microns or gauge, thickness affects durability and heat retention. Thicker materials often withstand higher temperatures and are less prone to deformation during transportation.
Dimensions: The size of the container should correspond to the volume of food it will hold. Standard sizes are widely available, but custom dimensions can be ordered depending on your product requirements.
Sealing Capability: Some containers come with lids or sealing options that enhance freshness and prevent contamination. Assess whether your application requires airtight seals or if simple covers suffice.
Temperature Resistance: Goldshine Ensure that the containers are suitable for the intended temperature range, whether for freezing, baking, or reheating.
Recyclability: As sustainability becomes increasingly important, consider containers that are recyclable and made from eco-friendly materials. This aligns with corporate responsibility goals and consumer preferences.
Quality evaluation is essential to ensure that aluminium foil containers meet safety and performance standards. Here are key points to consider during the inspection process:
Certification and Compliance: Look for products that hold certifications from recognized bodies such as SGS, TUV, or BSCI. These certifications indicate adherence to safety and quality standards.
Physical Inspection: Check for uniform thickness, any punctures, or defects in the material. A quality container should be free from holes or crumples that could compromise its integrity.
Sample Testing: Before committing to a large order, request samples to test their performance in real-world conditions. Assess how well they hold up under various temperatures and whether they maintain their shape during transport.
Supplier Reputation: Assess the manufacturer's track record in quality control and customer service. A reputable supplier like Goldshine, with over a decade of experience and a focus on stringent quality checks, can provide reliable products.
Aluminium foil containers serve a wide range of applications in various industries:
Food Service: Commonly used in restaurants and catering for takeaway meals, these containers are designed to retain heat and maintain food quality during transport.
Baking and Cooking: Many baking applications utilize aluminium foil containers for their ability to withstand high temperatures while ensuring even heat distribution.
Food Preservation: These containers are also effective for storing leftovers or pre-prepared meals, offering a barrier against moisture and air.
Understanding the specific needs of your application helps in selecting the right type of jumbo aluminium foil container. For instance, if you require containers for high-temperature baking, ensure that the chosen product is rated for such use.
Goldshine company has established an efficient response mechanism to ensure that customers can quickly get attention when they encounter problems. Customers can contact our after-sales team at any time through multiple channels, such as telephone, email, online customer service platform and so on. Once we receive customer feedback, we promise to make an initial response within one hour, understand the general situation of the problem, and inform the customers of the action steps we are about to take.
Aluminum foil has an extremely strong barrier ability against oxygen, water vapor, light rays and so on. In terms of food packaging, it can effectively prevent food from oxidizing, deteriorating, getting damp, and losing nutritional components or changing in flavor due to the influence of light.Aluminum foil can conduct heat rapidly and is widely used in cooking utensils. For example, aluminum foil paper used in baking can make food heated evenly, speed up the cooking process, and at the same time, it can also prevent food from getting burnt and sticking to the baking pan, which makes cleaning convenient.
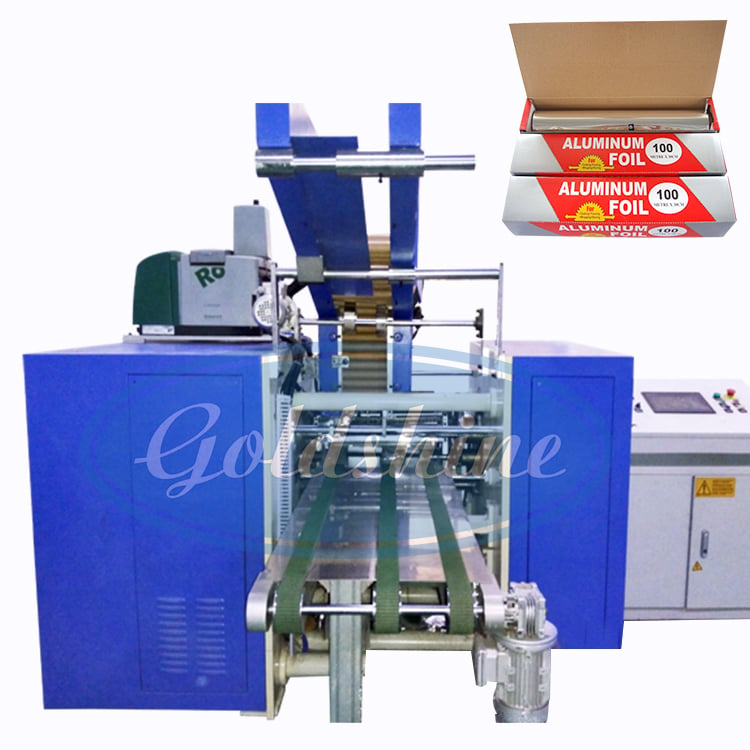
Zhangjiagang Goldshine Aluminum Foil Co., Ltd was established in 2010 and has over 14 years of experience in household aluminum foil production. With a land area exceeding 10,000 square meters, the company boasts a seasoned team in sales, production, quality inspection, research and development, and after-sales service, forming an integrated collaborative system. Our main products include aluminum foil rolls, aluminum foil sheets, aluminum foil containers, baking paper, cling film, aluminum foil rewinding machines, aluminum foil container making machines, aluminum foil packaging machines, and various other diversified products.
Aluminum foil itself is non-toxic and odorless, and complies with strict food safety and pharmaceutical packaging standards. When it comes into direct contact with various kinds of food and pharmaceuticals, it will not release harmful substances, thus providing a safe and reliable packaging environment for the products. Whether in the process of high-temperature sterilization or during long-term storage, aluminum foil can adhere to the safety bottom line and become an important safeguard for protecting consumers' health.
Goldshine stands out as a reliable supplier of aluminium foil container boxes due to its commitment to quality, innovation, and sustainability. With 14 years of experience in the industry, the company operates 26 advanced automated production lines, ensuring consistent output quality and the ability to meet large orders—typically producing 4-6 containers daily.
The company holds multiple certifications, including SGS, TUV, and BSCI, which affirm its adherence to international quality standards. Additionally, Goldshine places a strong emphasis on technological upgrades and sustainable practices, making it a forward-thinking partner in the manufacturing sector.
Furthermore, Goldshine offers customization capabilities to meet specific buyer requirements. Whether you need unique dimensions, designs, or packaging options, their team can assist in developing products tailored to your operational needs.
Selecting the right kitchen aluminium foil container box involves careful consideration of specifications, quality, and application suitability. By choosing a reputable manufacturer like Goldshine, you can ensure that your packaging solutions meet the highest standards while supporting your business's operational goals.
Copyright © Zhangjiagang Goldshine Aluminium Foil Co., Ltd. All Rights Reserved