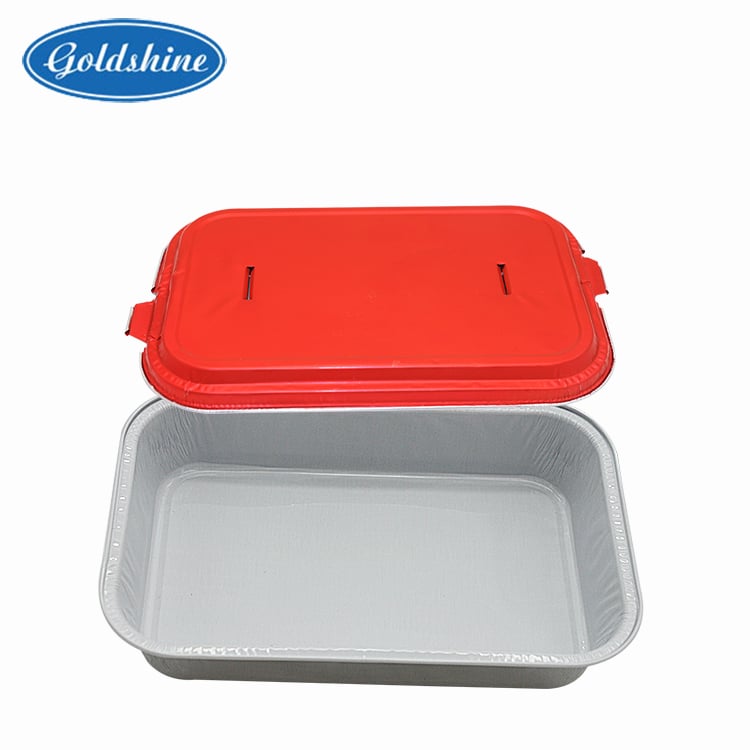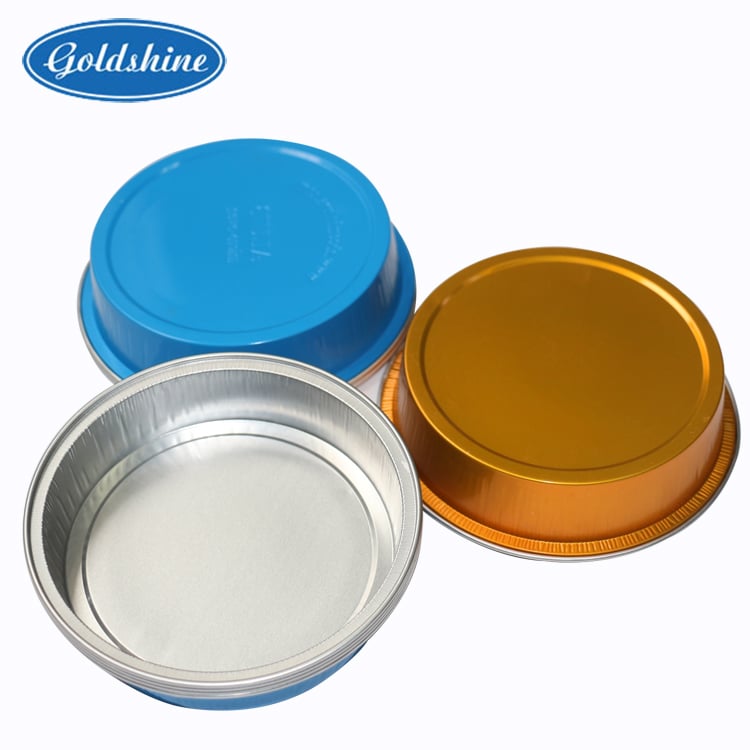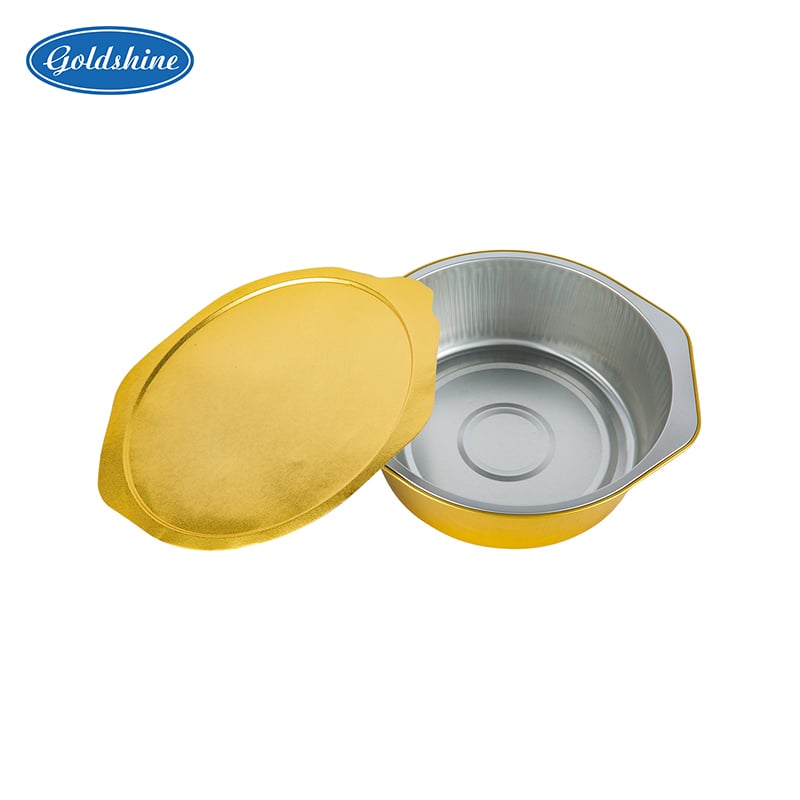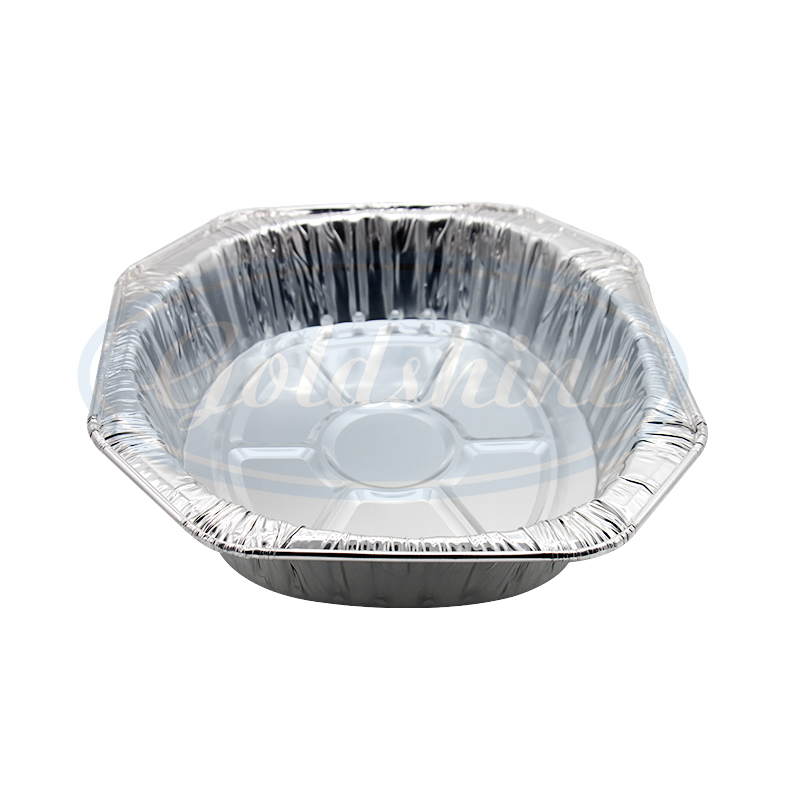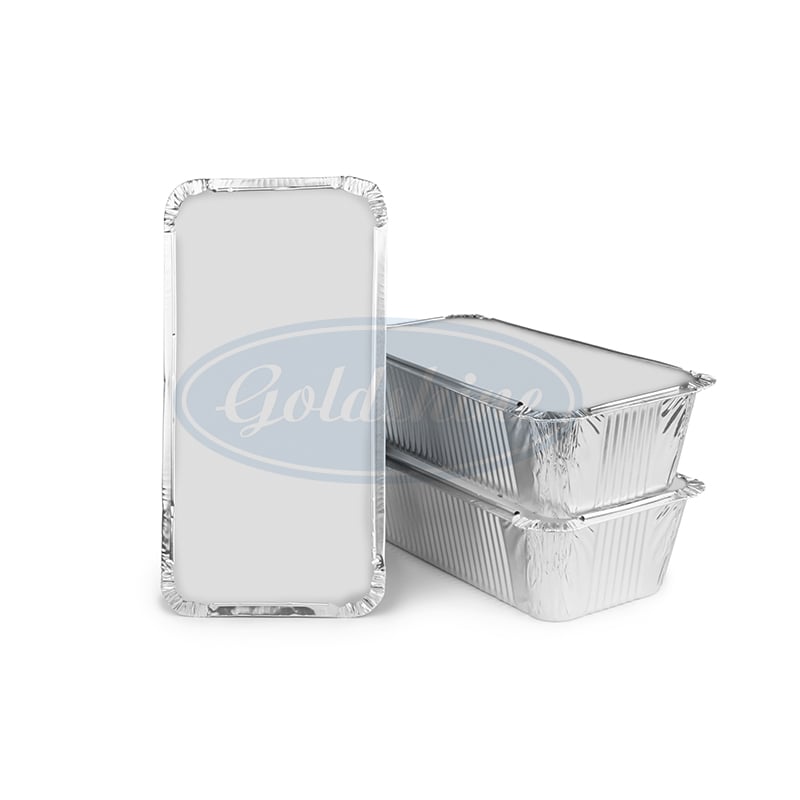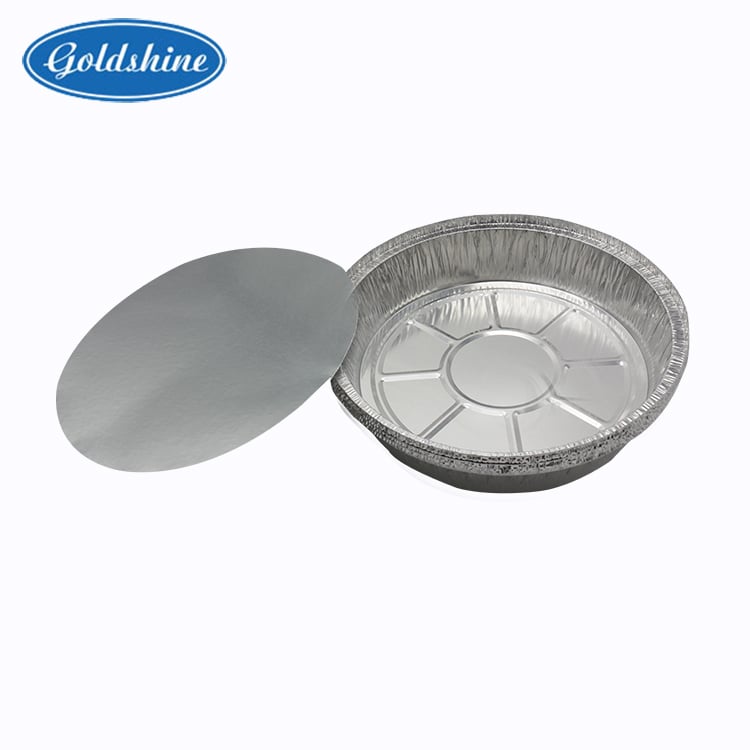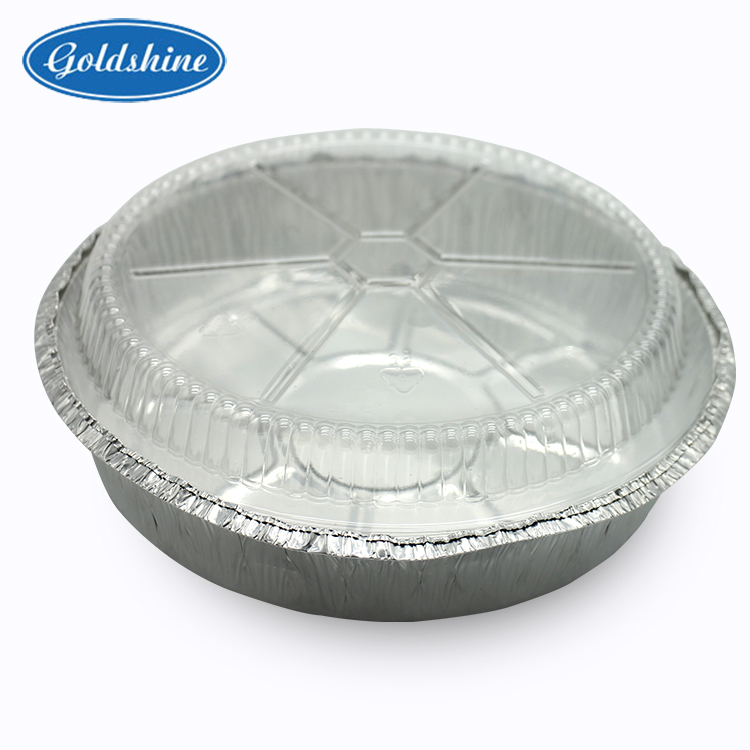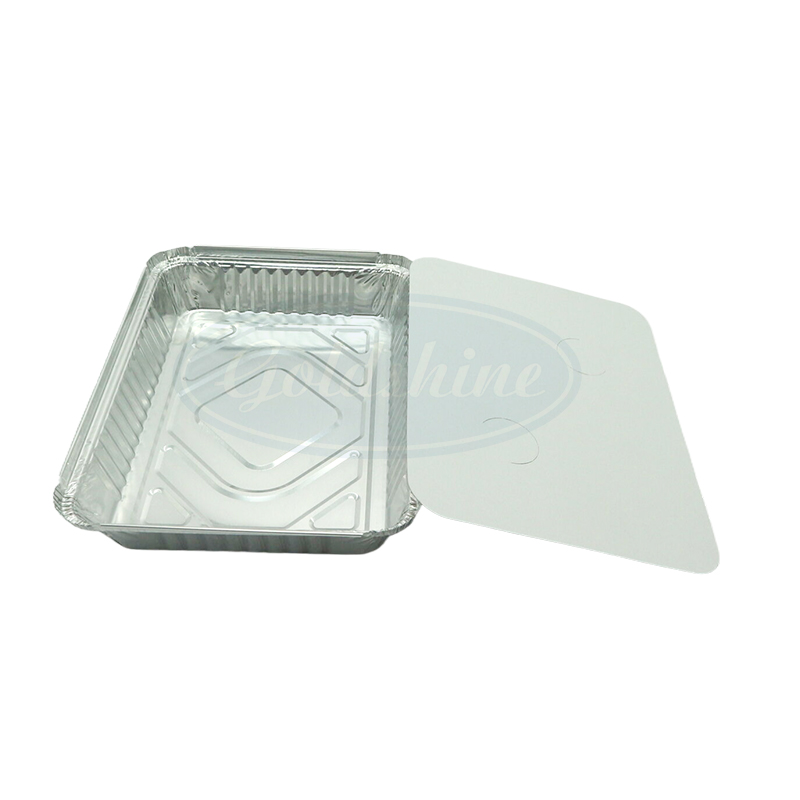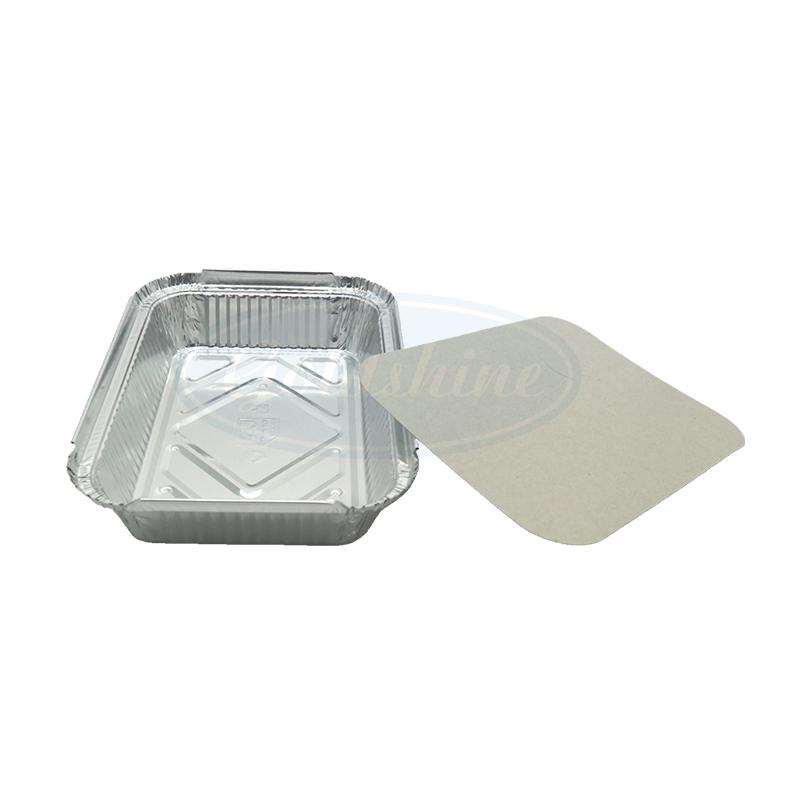
Aluminum containers for food are essential in the food packaging industry, offering durability, safety, and versatility. As a B2B buyer, understanding the specifications and qualities of these containers is crucial for making informed purchasing decisions. This article will explore how to choose high-quality aluminum container making machine, identify reliable suppliers, discuss essential specifications, address common issues, and highlight applications in food packaging and preservation.
When selecting aluminum containers for food applications, several key factors should be considered. First, evaluate the material quality. Containers made from food-grade aluminum are essential to ensure safety and compliance with health regulations. Look for containers that are free from harmful chemicals and have certifications such as SGS, TUV, or BSCI, which indicate adherence to global safety standards.
Next, consider the container's design and structure. The container should be lightweight yet robust, able to withstand transportation and handling without compromising integrity. Features such as airtight seals enhance food preservation, while easy stacking designs can optimize storage efficiency.
Additionally, assess the manufacturer's quality control processes. A reliable supplier, like Zhangjiagang Goldshine Aluminum Foil Co., Ltd, adheres to strict quality checkpoints throughout production, ensuring that every round aluminum containers with lids meets safety and performance expectations.
Finding trustworthy suppliers is vital for consistent quality and supply reliability. Look for manufacturers with extensive experience in the aluminum packaging industry, preferably those who have been in operation for over a decade and have a proven track record of exporting to various global markets.
Engage with suppliers who possess relevant certifications that indicate compliance with international standards, such as ISO certifications or food safety approvals like KOSHER. This not only assures quality but also reduces risks associated with product recalls or safety violations.
Furthermore, consider the supplier's production capabilities. Suppliers with advanced automated lines, like those found at Zhangjiagang Goldshine Aluminum Foil Co., Ltd, can offer higher production consistency and efficiency. Inquire about their minimum order quantities (MOQ) and lead times to ensure they can meet your specific demands.
When choosing aluminum containers, several specifications are crucial for ensuring functionality and safety:
Material Thickness: The thickness of the aluminum impacts the container's strength and heat resistance. Thicker materials typically provide better durability but may affect weight and cost. It's essential to balance these factors based on your specific application needs.
Dimensions: Accurate dimensions are critical for compatibility with existing equipment and storage solutions. Confirm that the container dimensions are suitable for your packaging process and can accommodate the required volume.
Sealing Mechanism: Depending on the application, consider whether the aluminum container with lid will be used for hot or cold food items. Containers designed for hot food should have heat-resistant seals to prevent leaks.
Barrier Properties: Evaluate the container's ability to prevent oxygen and moisture ingress. High-quality aluminum containers typically have coatings that enhance barrier properties, crucial for extending shelf life.
Customization Options: If branding or specific features are important, inquire about customization capabilities. This includes printing options, unique sizes, or shapes that may be necessary for your product.
B2B buyers should be aware of common issues that can arise with Goldshine aluminum containers and how to address them effectively:
Corrosion: Aluminum can corrode if exposed to certain acidic foods. Selecting containers with protective coatings can mitigate this issue. Always check the compatibility of the container material with the food being packaged.
Weak Seals: Poor sealing can lead to leaks. It is advisable to conduct tests on samples to ensure that the seals hold under pressure and thermal conditions. Always request samples before mass production to verify that seals meet your expectations.
Dimensional Variability: Inconsistent sizing can lead to packaging issues. Ensure that the supplier implements strict quality control measures to maintain dimensional accuracy throughout production.
Handling Damage: Containers may suffer from dents or damage during transportation. Discuss packaging and shipping methods with suppliers to minimize these risks, such as using cushioning materials or reinforced cartons.
Aluminum foil has an extremely strong barrier ability against oxygen, water vapor, light rays and so on. In terms of food packaging, it can effectively prevent food from oxidizing, deteriorating, getting damp, and losing nutritional components or changing in flavor due to the influence of light.Aluminum foil can conduct heat rapidly and is widely used in cooking utensils. For example, aluminum foil paper used in baking can make food heated evenly, speed up the cooking process, and at the same time, it can also prevent food from getting burnt and sticking to the baking pan, which makes cleaning convenient.
Zhangjiagang Goldshine Aluminum Foil Co., Ltd was established in 2010 and has over 14 years of experience in household aluminum foil production. With a land area exceeding 10,000 square meters, the company boasts a seasoned team in sales, production, quality inspection, research and development, and after-sales service, forming an integrated collaborative system. Our main products include aluminum foil rolls, aluminum foil sheets, aluminum foil containers, baking paper, cling film, aluminum foil rewinding machines, aluminum foil container making machines, aluminum foil packaging machines, and various other diversified products.
Aluminum foil itself is non-toxic and odorless, and complies with strict food safety and pharmaceutical packaging standards. When it comes into direct contact with various kinds of food and pharmaceuticals, it will not release harmful substances, thus providing a safe and reliable packaging environment for the products. Whether in the process of high-temperature sterilization or during long-term storage, aluminum foil can adhere to the safety bottom line and become an important safeguard for protecting consumers' health.
Goldshine company has established an efficient response mechanism to ensure that customers can quickly get attention when they encounter problems. Customers can contact our after-sales team at any time through multiple channels, such as telephone, email, online customer service platform and so on. Once we receive customer feedback, we promise to make an initial response within one hour, understand the general situation of the problem, and inform the customers of the action steps we are about to take.
Aluminum containers are widely used across various food service applications due to their versatility and effectiveness in preserving food quality. Common applications include:
Take-out and Delivery: Many restaurants and food service providers utilize aluminum containers for take-out and delivery options. Their lightweight nature and ability to maintain food temperature make them ideal for transporting meals.
Baking and Cooking: Aluminum baking trays and pans are popular in both commercial and home kitchens. They provide even heat distribution, which is essential for baking, while also being recyclable and easy to clean.
Food Storage: Aluminum containers are excellent for food preservation. They act as effective barriers against moisture and oxygen, which helps extend the shelf life of perishable items. This is particularly important for the food manufacturing sector.
Catering Events: For large-scale events, aluminum containers allow for efficient serving and cleanup. Their stackable design saves space, and they can often be used in ovens or freezers, enhancing their versatility.
In summary, understanding the specific qualities and capabilities of aluminum containers for food is crucial for effective purchasing decisions. By considering these factors, B2B buyers can ensure they select containers that not only meet their operational needs but also align with safety and quality standards.
Copyright © Zhangjiagang Goldshine Aluminium Foil Co., Ltd. All Rights Reserved